

Rather than rely on off-site storage, with its added logistical complexity, increased staffing needs, leasing costs, and operational risk, they partnered with Morrison Industrial Equipment to redesign their facility layout, implementing a racking solution that increased their storage capacity by 80%.
The Problem
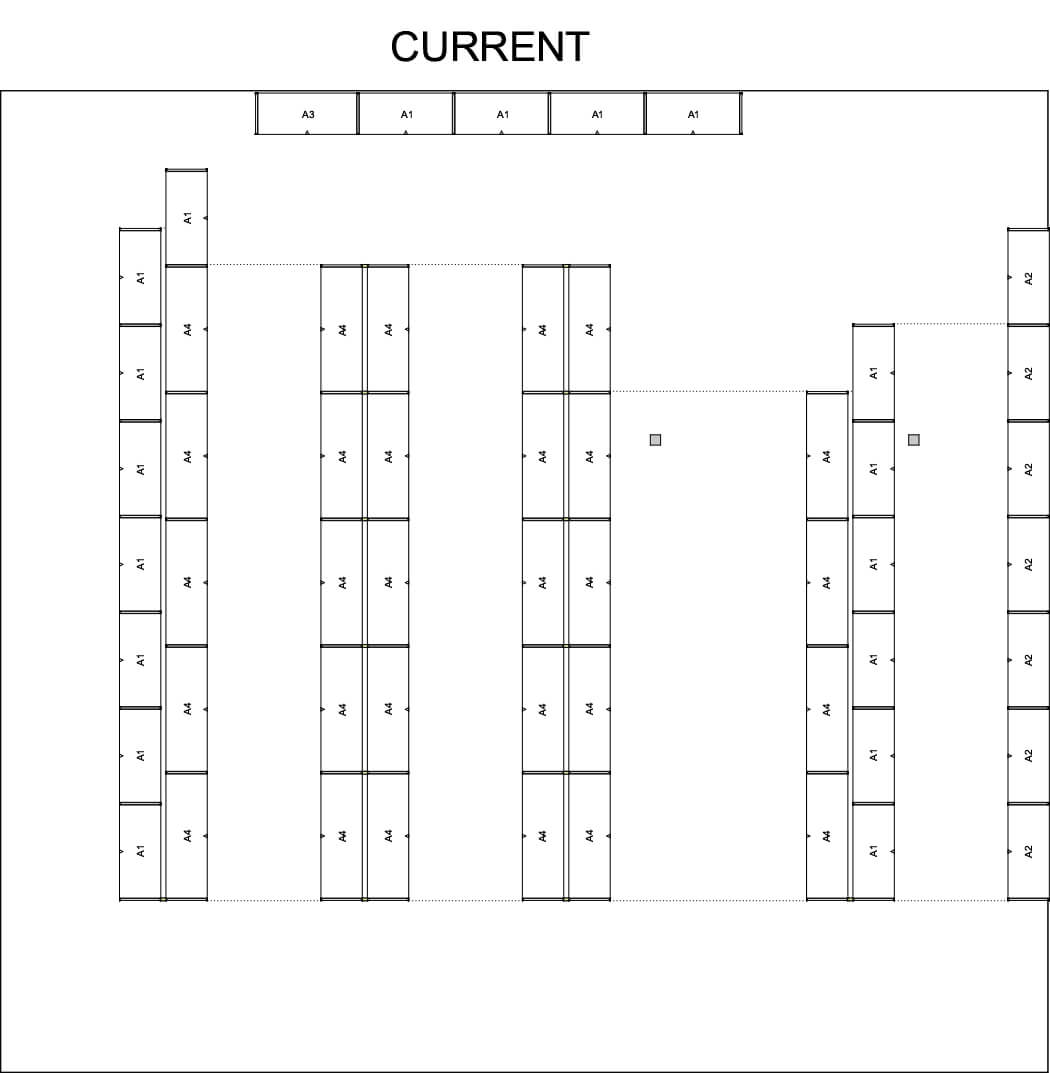
With approximately 580 pallet positions, the warehouse was struggling to support daily operations. A wide range of products were stored in the space, many requiring direct pallet access at all times. The combination of high product variety and constant accessibility demands created workflow inefficiencies, disorganization, and difficulty maintaining accurate inventory counts. With the company continuing to grow, it became clear that the existing layout could not scale without a comprehensive storage redesign.
The Solution
To maximize space utilization, the warehouse was reconfigured and expanded by 14 feet. The added footprint, combined with narrower aisles and an additional vertical rack level, created more than 450 new pallet positions, an 80% capacity gain.
Materials previously spread across multiple warehouse areas were consolidated into a single, organized cage space. A selective racking system ensures direct access to every pallet, improving accessibility without sacrificing density.
By centralizing inventory and refining pallet selectivity, the operation strengthened inventory oversight while reducing the number of operators needed to manage the area.

The Results
The redesigned warehouse now supports more than 1,000 pallet positions within the same footprint, positioning the company to accommodate continued growth onsite. Improved space utilization, material consolidation, and full pallet access provide greater inventory accuracy and a more efficient production environment.

